About Us
Our Mission. Your Health.
Our Mission. Your Health.
Our innovative company was established in 2019 at Sialkot. It is a part of ISLAM GROUP OF COMPANIES, the major stakeholder in the health and education sector of this country. Our aim is to become the leading, reputable and reliable pharmaceutical industry.
Islam Pharmaceuticals is a growing pharmaceutical company of Pakistan specializing in the formulation, development, manufacturing and marketing of a wide range of high-quality, economical medicines. We are a manufacturer and distribution network committed to delivering a high standard of services to our partners in the health care sector.
We lead with the highest standards, ensuring that medicines and consumer care products meet the needs of the community today, and we build capabilities to raise healthcare standards to meet the needs of future generations. Our aim is to become the #1 innovative, integrated pharmaceutical solution provider to the global pharmaceutical industry.

Our Vision
Our vision is to become the number 1 Global Healthcare Organization through building total Brand value, Innovation, Quality and Competence by 2025. A leading pharmaceutical provider in the industry by assuring high quality standards, better and more complete h...
Our Mission
To lead the healthcare industry with a dedicated mission to contribute towards the enrichment of quality of life around the world through the creation of innovative pharmaceuticals with unconventional thinking. We are also determined to become the most efficie...
Our Values
Ethics, integrity, professionalism, quality of service, innovation, and trust are our core values. These values are implemented in every aspect of the company and combined with our deep understanding of the market, sophisticated management knowledge, state-of-...
State of the Art Manufacturing
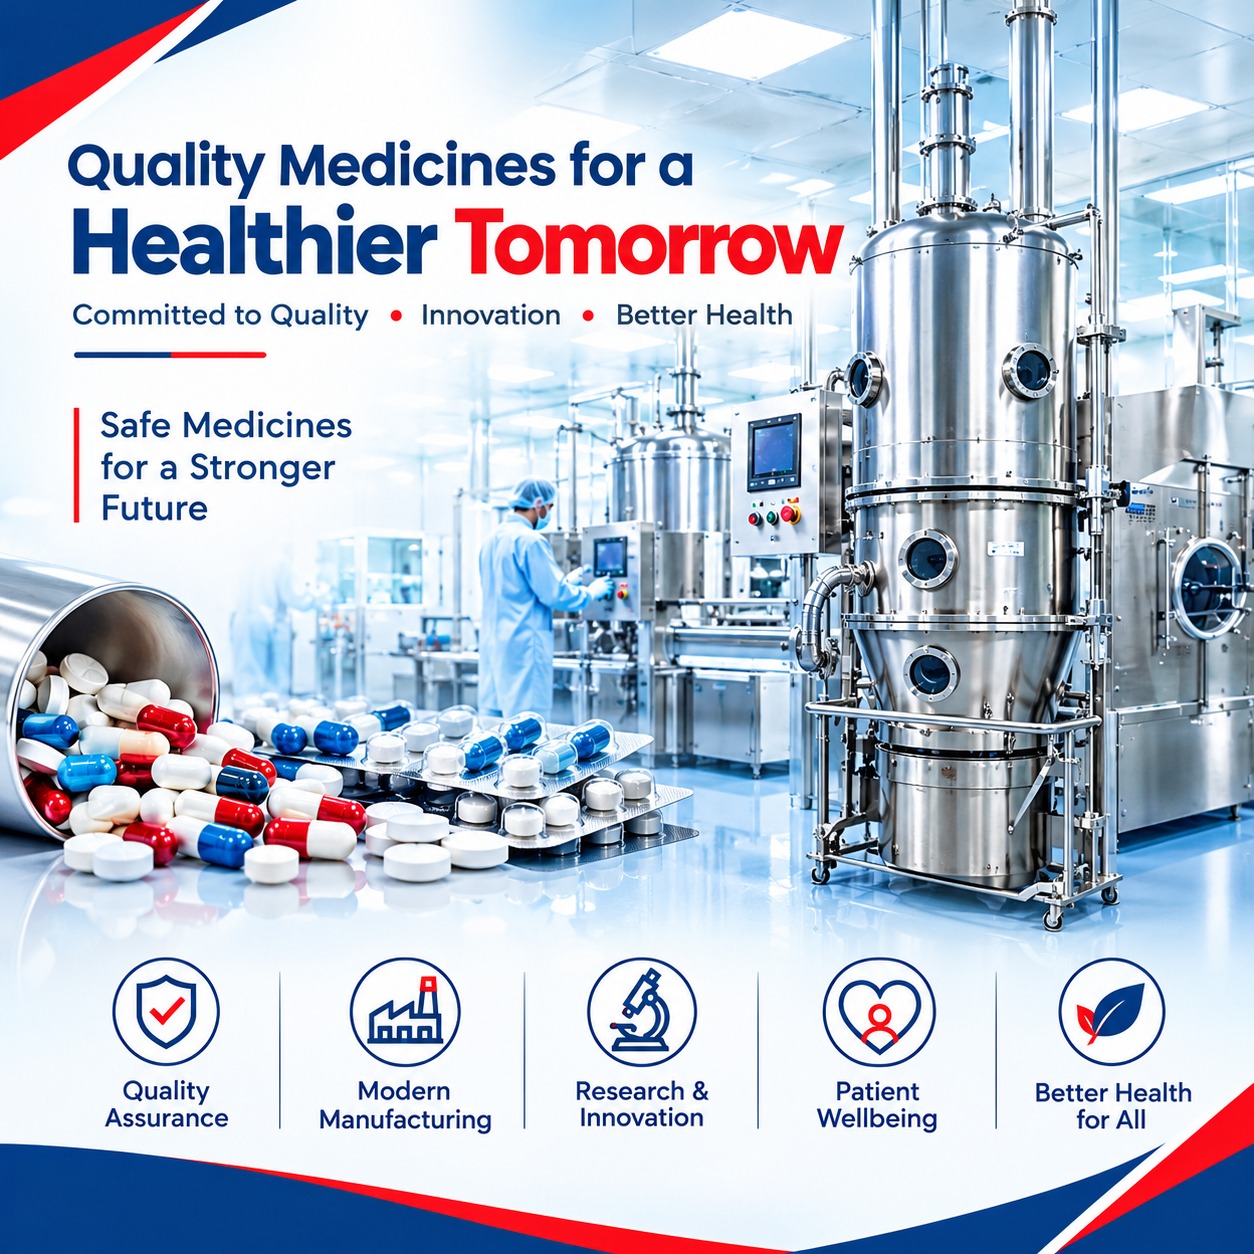
Islam Pharmaceuticals has state of the art manufacturing equipment and R&D facilities in strict adherence to cGMP standards — especially a Rapid Mixer Granulator, HEPA-filtered Fluidized Bed Dryer and automatic coating pan, along with GMP model compression machines, an automatic capsule filler equipped with metal detector, multidirectional motion mixers and blister machine.
The processing water is supplied through 316 SS loops after being purified by double pass RO membranes. Oil and moisture free compressed air is supplied by an oil free air compressor (Atlas Copco), passed through an air dryer and ultimately through filters.
Our dedication to quality in every medicine we produce is uncompromising and covers every stage of manufacturing. All equipment is calibrated and certified and every manufacturing process is validated. All manufacturing areas are epoxy covered, and all supplies are equipped with terminal H13 HEPA filters to avoid the risk of cross contamination. Active pharmaceutical ingredients are imported from US FDA approved sources worldwide.
What Drives Us
Quality Assurance
Calibrated equipment, validated processes.
Innovation
Creating pharmaceuticals with unconventional thinking.
Integrity & Trust
Ethics and professionalism in everything we do.
Global Sourcing
APIs from US FDA approved sources worldwide.
High Quality Standards
Strict cGMP compliance at every stage.
97% Satisfaction
Customer satisfaction rate across our partners.
Wide Product Range
Multi-vitamins, pain management and antibiotics.
Modern Facility
State of the art equipment and R&D facilities.
Patient First
Health and wellness — because every life matters.